Join World's Fastest Growing B2B Network
Join World's Fastest Growing B2B Network

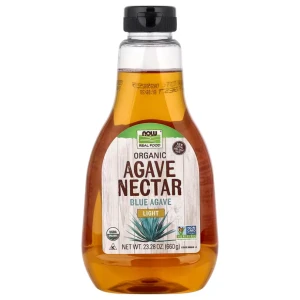


| MOQ | 1 Bottles |
| Port | Thailand |
| Packaging | Standard |
| Lead Time | 7-15 Days |
| Product Name | Agave syrup | Type | Natural Sweetner |
| Grades | Light / Amber / Dark | Taste | Mild to caramel-like depending on grade |
| Shelf Life | 12 – 24 months |
Agave syrup is a natural, plant-based liquid sweetener extracted from the sap of the agave plant. Known for its smooth consistency, mild flavor, and excellent solubility, it is widely used as an alternative to conventional refined sugar in food processing, beverage manufacturing, bakery production, and retail food markets.
Our premium agave syrup is carefully processed to maintain consistent sweetness, quality, and texture. With its versatile applications and growing demand in international markets, it is a suitable ingredient for food manufacturers, wholesalers, distributors, and retail brands seeking a reliable natural sweetener.
Agave syrup is produced by extracting juice from the core of the agave plant, followed by filtration, controlled heating, and concentration to achieve its characteristic honey-like consistency. The resulting syrup offers a smooth texture and blends easily into a wide range of food and beverage products.
It is commonly used in both commercial and household applications as a plant-derived sweetening ingredient and is particularly popular among manufacturers developing vegan-friendly and alternative sweetener products.
Natural Plant-Based Ingredient: Derived from agave plants and suitable for applications requiring plant-based sweeteners.
Mild and Balanced Flavor: Offers a light, smooth taste that complements various food and beverage formulations.
Excellent Solubility: Easily dissolves in hot and cold liquids, making it suitable for different manufacturing processes.
Consistent Texture: Features a smooth, pourable consistency for convenient handling and processing.
Multiple Applications: Suitable for beverages, bakery products, confectionery, packaged foods, and industrial food production.
Quality-Controlled Processing: Manufactured under controlled processing conditions to maintain product consistency and quality.
We offer different varieties of agave syrup to meet the requirements of food manufacturers, distributors, and commercial buyers.
Light Agave Syrup
Mild and delicate flavor profile
Light color and smooth consistency
Ideal for tea, coffee, juices, smoothies, and beverage production
Amber Agave Syrup
Medium flavor intensity
Richer color and balanced sweetness
Suitable for baking, cooking, sauces, and desserts
Dark Agave Syrup
Deep color with a stronger, caramel-like flavor
Rich taste profile
Suitable for confectionery, specialty food products, and industrial food applications
Agave syrup primarily consists of naturally occurring sugars, including fructose and glucose. Its nutritional composition may vary depending on the agave variety and processing method.
Typical characteristics include:
Naturally occurring carbohydrates and sugars
Predominantly fructose-based sugar composition
Small amounts of trace minerals, depending on processing
No fat or cholesterol
Commonly marketed as an alternative sweetener to conventional sugar
Agave syrup is primarily valued for its sweetening properties and functional applications rather than as a significant source of nutrients.
Our agave syrup follows a controlled production process designed to achieve the desired sweetness, purity, and consistency.
Harvesting: Mature agave plants are selected and harvested.
Sap Extraction: Juice is extracted from the core of the agave plant.
Filtration: The extracted liquid is filtered to remove unwanted impurities.
Carbohydrate Conversion: Controlled enzymatic or thermal processing converts complex carbohydrates into simpler sugars.
Concentration: The filtered liquid is concentrated to achieve the required syrup consistency.
Quality Inspection: The finished product is evaluated for sweetness, color, purity, and viscosity.
Packaging: The syrup is filled into suitable hygienic containers for domestic distribution and international export.
Agave syrup is a versatile ingredient used across several commercial sectors.
Food and Beverage Manufacturing
Tea, coffee, and flavored drinks
Smoothies, juices, and nutritional beverages
Cocktails and beverage concentrates
Ready-to-drink beverage formulations
Bakery and Confectionery
Cakes, pastries, and muffins
Cookies and biscuits
Desserts and sweet toppings
Candy and confectionery manufacturing
Health and Wellness Food Products
Plant-based sweetener formulations
Vegan food products
Alternative sweetener blends
Specialty food and beverage products
Industrial Food Processing
Breakfast cereals and granola
Energy bars and snack products
Sauces, dressings, and condiments
Packaged and processed food products
Plant-Based Sweetening Solution: Suitable for vegan food formulations.
High Sweetening Capacity: Its sweetness can allow manufacturers to use smaller quantities compared with conventional sugar, depending on the formulation.
Easy Integration: Blends conveniently into liquid and semi-liquid food products.
Versatile Commercial Applications: Suitable for manufacturers across multiple food and beverage categories.
Flexible Supply Options: Available in different grades and packaging formats to accommodate retail, wholesale, and industrial requirements.
International Market Potential: Increasing interest in alternative sweeteners creates opportunities across global food and beverage markets.
We offer flexible packaging solutions to accommodate different order quantities and buyer requirements.
250 ml – 500 ml: Retail bottles for supermarkets and consumer markets.
1 L – 5 L: Food-service containers for restaurants, bakeries, and commercial kitchens.
Bulk Drums: Suitable for industrial manufacturers and large-volume buyers.
Private Label Packaging: Customized branding and labeling options.
Export Packaging: Properly sealed containers suitable for international transportation and distribution.
Custom packaging specifications and bulk order requirements can be discussed according to buyer needs.
To maintain product quality throughout storage and distribution:
Store in a cool and dry environment.
Keep containers tightly sealed after opening.
Protect the product from direct sunlight and excessive heat.
Use clean and hygienic dispensing equipment.
Follow the recommended storage conditions provided on the product label.
369/2, Soi Duang Di, Sukhumvit Road, Noen Phra Subdistrict, Mueang Rayong District, Rayong Province
One moment please
 Member's Area
 Messages
 Need Help



 Browse Through Millions of High-Quality Products.